A rugged enclosure can look uncomplicated from the outside. A moulded shell, a seal, some fixings and the electronics inside.
In practice, the enclosure sits at the point where industrial design, electronics, material behaviour, tooling and the operating environment meet. A decision made in one area can create a problem somewhere else. A pigment can affect RF transmission. A gate position can create warpage. A tool designed sensibly for launch volumes can become inefficient when demand grows.
Around 65% of Dudley Associates’ business concerns enclosures, primarily across oil and gas, rail, defence and navigation, and electronics. The following examples show four engineering decisions that can reduce risk before and after a rugged device enters production.
1 Treat material selection as an engineering exercise
An oil and gas customer recently asked us to support the material strategy for a suite of new P20 steel tools. The customer understood CAD and tooling well, but the enclosure had a demanding set of environmental requirements.
The polymer needed to offer outdoor weatherability and UV resistance, a defined UL94 flame classification, chemical and solvent resistance, and performance in a seawater environment. The difficulty was not finding separate datasheet claims. It was establishing whether one practical material and colour system could satisfy the complete application at the proposed wall thickness.
A Covestro PC/PBT blend has been identified as a candidate. The work now involves confirming the exact listings and exposure requirements before the material and tooling assumptions are treated as fixed.
This is an important distinction. Material selection should not be reduced to finding a polymer with the right headline properties. Shrinkage, flow, moisture sensitivity, gate design and dimensional stability all influence whether that polymer will work in the actual component.
2 Remember that colour can affect product performance
For a rugged navigation system, we developed an insert-moulded and overmoulded component using a Makroblend PC/PBT substrate and a Kraiburg TPE.
The device required RF transparency. That made the masterbatch part of the functional specification, not simply the colour specification. Standard pigmentation often relies on carbon, while some other colours can include metallic content. Either can influence RF behaviour in sensitive applications.
A bespoke masterbatch was therefore sourced without carbon or metallic constituents. The component progressed through drop testing and was validated, with the first production order now approaching.
The development timeline was also tightly controlled. Following DFM approval, the 1+1 aluminium tool was manufactured within four weeks. T0 followed one week later and T1 components were available the week after that.
3 Let simulation challenge a frozen design
Another electronics customer approached us with a design considered ready for tooling. The expected volumes supported an aluminium tool, and there was little appetite for unnecessary feature changes.
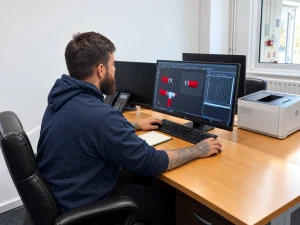
Early Moldex3D analysis showed that the original feed arrangement did not fill the component properly. Adjusting the processing assumptions could make the cavity appear full, but the predicted warpage remained significant.
Several alternatives were simulated. The most effective route involved flipping the component in the tool and feeding from the underside through the area around existing insert-pin holes. The revised strategy improved the predicted filling and warpage result without forcing a wholesale redesign.
The DFM is approved and the tool is progressing towards T1. Physical sampling will determine how closely the moulded result follows the simulation, but the risk was identified while there was still time to act without modifying finished tooling.
4 Allow tooling to evolve when demand changes
Tooling is normally specified against an expected production volume. The sensible answer for a new concept may not remain the sensible answer after commercial success.
A warehouse-management technology customer came to Dudley around five years ago with a locker system for handheld scanners. We manufactured eight tools around the needs and volumes understood at the time. Some components used loose inserts, avoiding the initial cost of more complex automated features.
As demand grew, the manual handling associated with those inserts became more significant. We modified the component and tooling so that sliders could replace the loose inserts. The change shortened the moulding cycle and allowed the repeat-part cost to be reduced.
The next review concerns material and colour variants for different end users. Because a change in polymer can also change shrinkage, cavitation and finished dimensions are being considered before the variant is released.
Rugged performance comes from connected decisions
These projects concern different markets and different products, but the underlying lesson is consistent. Rugged performance is not created by selecting a strong plastic after the design is complete.
It comes from connecting the operating environment, material evidence, component geometry, mould filling, tool construction, testing and production volumes. It also means revisiting earlier decisions when the product or commercial requirement changes.
For a moulder, the useful question is not simply whether the part can be produced. It is whether the proposed material, design and tooling route can produce it repeatedly, at the required quality and at a cost appropriate to the product’s stage.
Bring manufacturing evidence into the project earlier
If you are developing a rugged enclosure or reviewing an existing product, Dudley Associates can provide an initial feasibility review covering material, mouldability and tooling risk. Send us your CAD, specification or early concept and we will help identify the questions that should be resolved before production tooling begins.
Frequently asked questions
What makes an electronic enclosure rugged?
Ruggedness depends on the operating environment. Requirements may include impact resistance, sealing, UV stability, chemical exposure, temperature, flame performance, dimensional control and reliable assembly.
When should a moulder become involved?
Ideally before the product design and material specification are fully frozen. Early involvement provides more options for resolving wall thickness, gating, warpage, sealing and tooling risks.
Can mould flow analysis replace physical trials?
No. Simulation helps identify risk and compare alternatives, but T0, T1 and application testing remain essential.
Can an existing mould tool be modified for higher volumes?
Often, yes. Tool condition, original construction and part geometry determine whether automation, improved cooling, revised ejection or other modifications are practical.
Why does the masterbatch need to be validated?
A masterbatch changes more than colour. Its carrier resin, pigment and additives can affect compatibility, appearance, mechanical properties, compliance and, in some applications, RF performance.